
Kynar 500 is the industry standard for protecting metal surfaces against harsh environmental conditions. It is a high-performance PVDF (polyvinylidene fluoride) resin-based coating system that holds its appearance and protective properties for over 30 years.
Arkema developed the coating, which contains a minimum of 70% PVDF resin. That resin content creates a strong molecular bond that resists UV radiation, chemicals, and extreme weather.
What Is Kynar 500? Technical Composition
The science behind Kynar 500 explains why it outperforms conventional coating systems on metal roofing, and why that gap matters once the roof is actually installed. A carefully engineered molecular structure is what makes the difference.
Table 1: Chemical Composition
| Component | Percentage | Function |
| PVDF Resin | 70% minimum | Primary protective polymer |
| Acrylic Resins | 20-30% | Adhesion and flexibility |
| Pigments | 2-5% | Color and UV protection |
| Additives | 1-3% | Performance enhancers |
PVDF’s molecular structure features alternating carbon-fluorine bonds, among the strongest chemical bonds in organic chemistry. That fluoropolymer arrangement resists UV degradation, which is what causes conventional coatings to fade, chalk, and break down over time.
Manufacturing involves precise resin production under tight quality control, specialized pigment integration for uniform dispersion, and strict application specifications for consistent performance.
The 70% minimum PVDF content is what separates Kynar 500 from standard paint systems. Lower concentrations hurt performance fast: coatings with 50% PVDF last only half as long, and anything below 30% offers barely any advantage over traditional paint. That 70% threshold is what forms a continuous fluoropolymer matrix, giving the coating comprehensive protection instead of scattered pockets of resistance.
5 Key Benefits of Kynar 500 Coatings
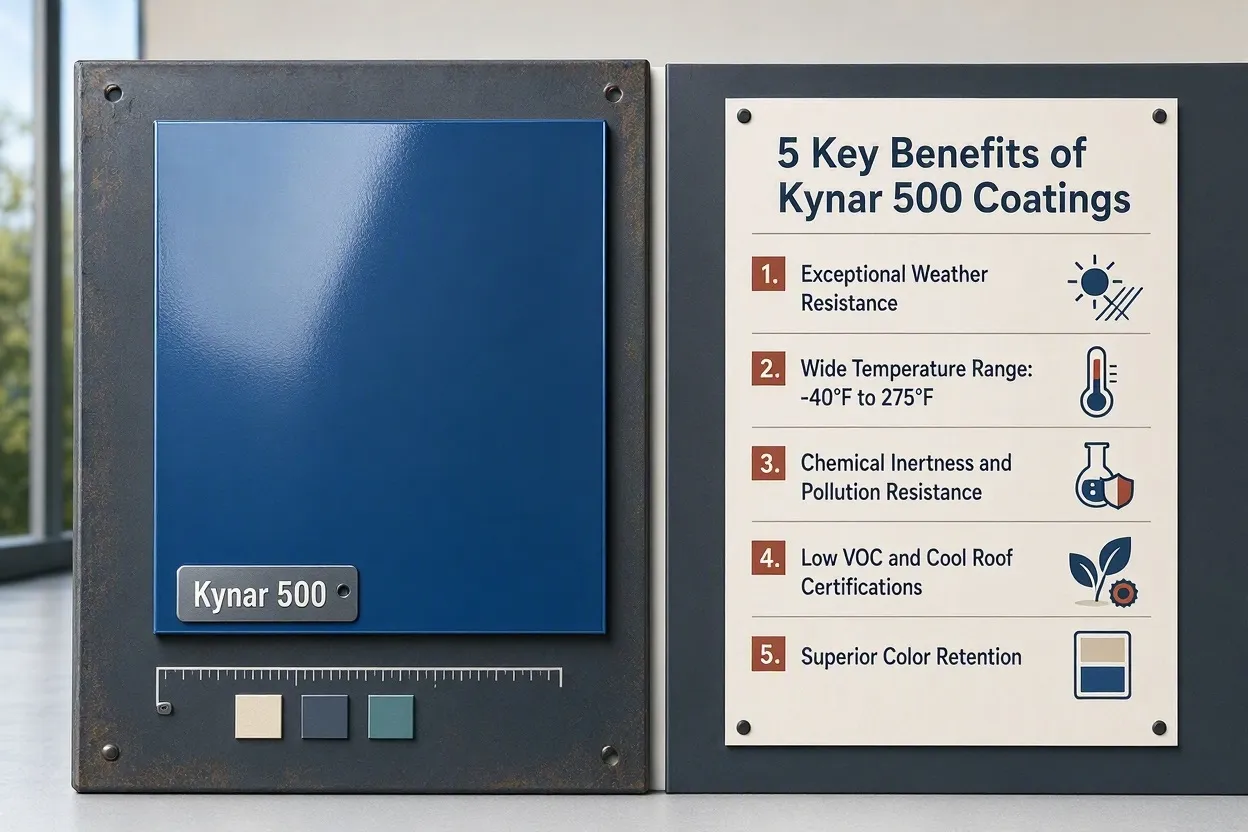
Exceptional weather resistance. The fluoropolymer bonds don’t break down under solar exposure. Per Arkema’s published specifications, the coating performs from -40°F (-40°C) to 275°F (135°C) without cracking or delamination, and it resists acid rain and pollution through chemical inertness. Low-VOC formulations also meet strict environmental regulations, and cool roof certifications cut urban heat island effects.
Superior color retention. Kynar 500 keeps 95% color integrity over 20 years, with Delta E measurements typically below 5 units, according to manufacturer testing data. Delta E readings give an objective measure of that stability, and the wide color palette means design flexibility doesn’t come at the cost of performance.
Chemical and corrosion resistance. The coating protects against industrial chemicals, including acids, bases, and solvents. In salt spray testing for coastal applications, manufacturer data shows it exceeds 4,000 hours, and the impermeable barrier it forms prevents oxidation and rust.
Self-cleaning properties. The hydrophobic surface causes water to bead and roll off, taking dirt and debris with it. That shedding capability cuts staining and buildup, which means lower maintenance costs over time.
Long-term warranty coverage. Kynar 500 typically carries a 30-year fade and chalk warranty plus a 20-year adhesion guarantee, so the coating won’t peel or flake. Film integrity coverage also protects against cracking and checking, and fewer repainting cycles over that span mean lower lifecycle costs, a point covered in more detail in the ROI section below.
Kynar 500 vs. Other Coating Systems
Kynar 500 outperforms competing coating systems on nearly every measurable metric, despite a higher upfront cost.
Coating System Comparison
| Coating Type | Lifespan | Color Retention | Cost Index | Warranty |
| Kynar 500 PVDF | 30-40 years | Excellent (ΔE<5) | High | 30 years |
| Hylar 5000 PVDF | 30-40 years | Excellent (ΔE<5) | High | 30 years |
| SMP (Silicone Modified) | 20-30 years | Good (ΔE<10) | Medium | 20 years |
| Polyester | 10-20 years | Fair (ΔE<15) | Low | 10 years |
| Acrylic | 7-15 years | Poor (ΔE>15) | Very Low | 5-10 years |
The gap shows up clearly in chalk resistance: Kynar 500 holds ratings of 8-10 after 20 years, versus 4-6 for SMP and 1-3 for polyester. Gloss retention tells a similar story. Kynar 500 keeps 80% of its initial gloss after two decades, while polyester drops below 30%. Thermal cycling and mechanical stress testing show the same pattern in flexibility and adhesion.
Over a 30-year span, Kynar 500 needs zero recoats, compared to three for polyester systems and two for SMP. Once labor, downtime, and materials are factored in, total cost favors Kynar 500 by 40-60%. That’s why it’s the standard recommendation for high-visibility projects, coastal environments, and buildings where maintenance access is limited or expensive.
5 Primary Applications of Kynar 500
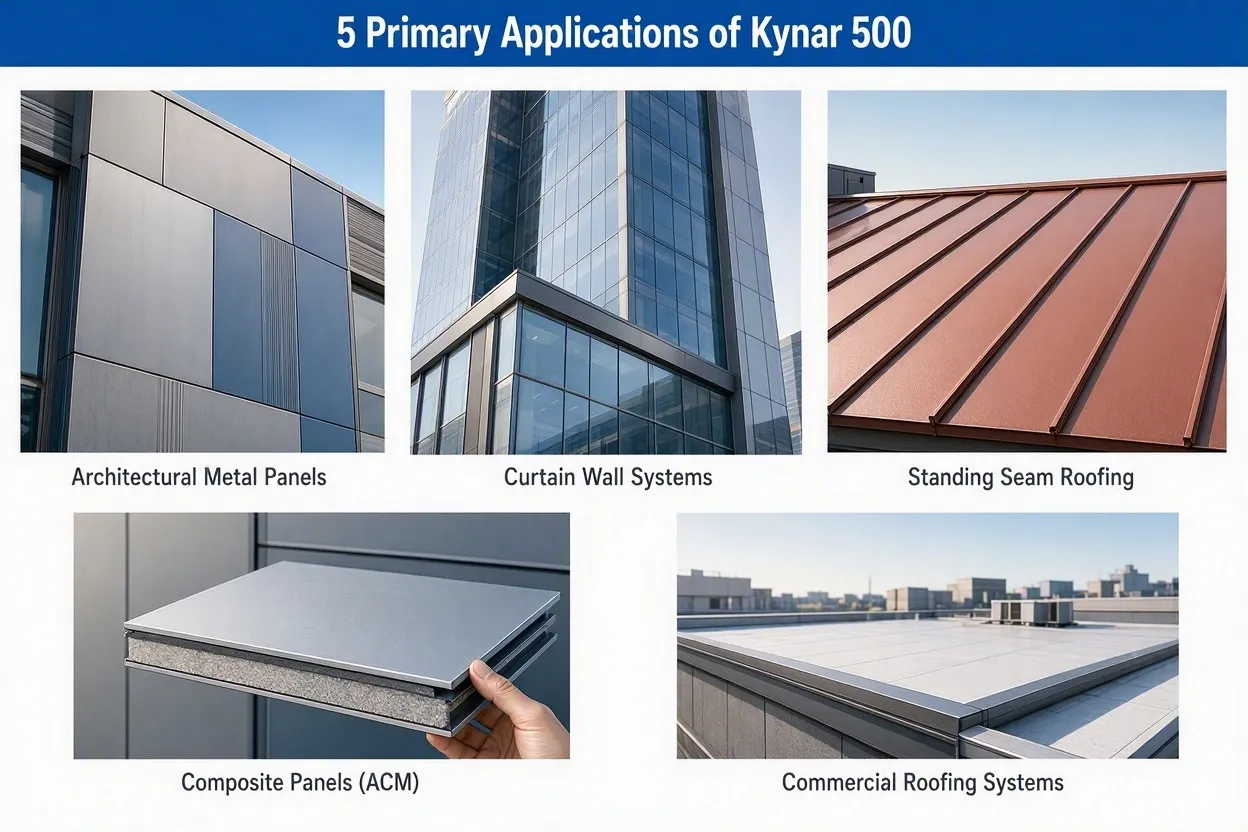
Architectural metal panels. Curtain wall systems on skyscrapers need decades of maintenance-free performance. Standing seam roofing depends on weather resistance and long-term aesthetics, and composite panels (ACM) used on modern facades rely on color stability.
Commercial roofing systems. Cool roof applications reduce building energy consumption, and reflective properties help energy-efficient buildings meet certification requirements, including LEED credits.
Industrial facilities. Chemical processing plants need resistance to corrosive vapors and spills. Coastal installations face constant salt spray, and high-corrosion environments demand maximum protection.
Transportation industry. Aircraft components need lightweight, durable protection. Rail car exteriors have to withstand weather extremes and chemical exposure, and marine applications need resistance to saltwater and UV damage.
Specialty applications. Solar panel frames need to hold their appearance while maximizing energy output. Satellite dishes have to keep a precise shape without coating degradation, and outdoor furniture and fixtures stay attractive despite constant exposure.
Installation and Application Process
Kynar 500 only delivers its full performance when installation follows strict specifications from start to finish.
Surface preparation comes first. Cleaning has to remove oils, oxidation, and contaminants that would otherwise compromise bonding. Primer specifications ensure compatibility between substrate and topcoat, with chrome-free options available for projects that need environmental compliance. Quality control checks verify surface profile, cleanliness, and primer thickness before the topcoat goes on.
The application method depends on the project and substrate. Coil coating, a continuous process, gives the most consistent results for flat stock, with tight temperature and speed control ensuring even coverage. Spray application, done in the field, handles complex geometries but needs experienced applicators and a controlled environment. Electrostatic application maximizes transfer efficiency and gives strong edge coverage.
Coating thickness affects long-term performance. Standard applications call for 0.8-1.2 mils, which balances protection against cost. Severe environments call for 1.5-2.0 mils. Multi-coat systems build up thickness while maintaining adhesion between layers.
Curing activates the coating’s protective properties through controlled thermal processing. Temperatures of 450-500°F (232-260°C) achieve full resin fusion without degrading the material. Cure time typically runs 40-60 seconds at peak metal temperature, and applicators verify a complete cure through solvent resistance and adhesion testing.
Cost Considerations and ROI
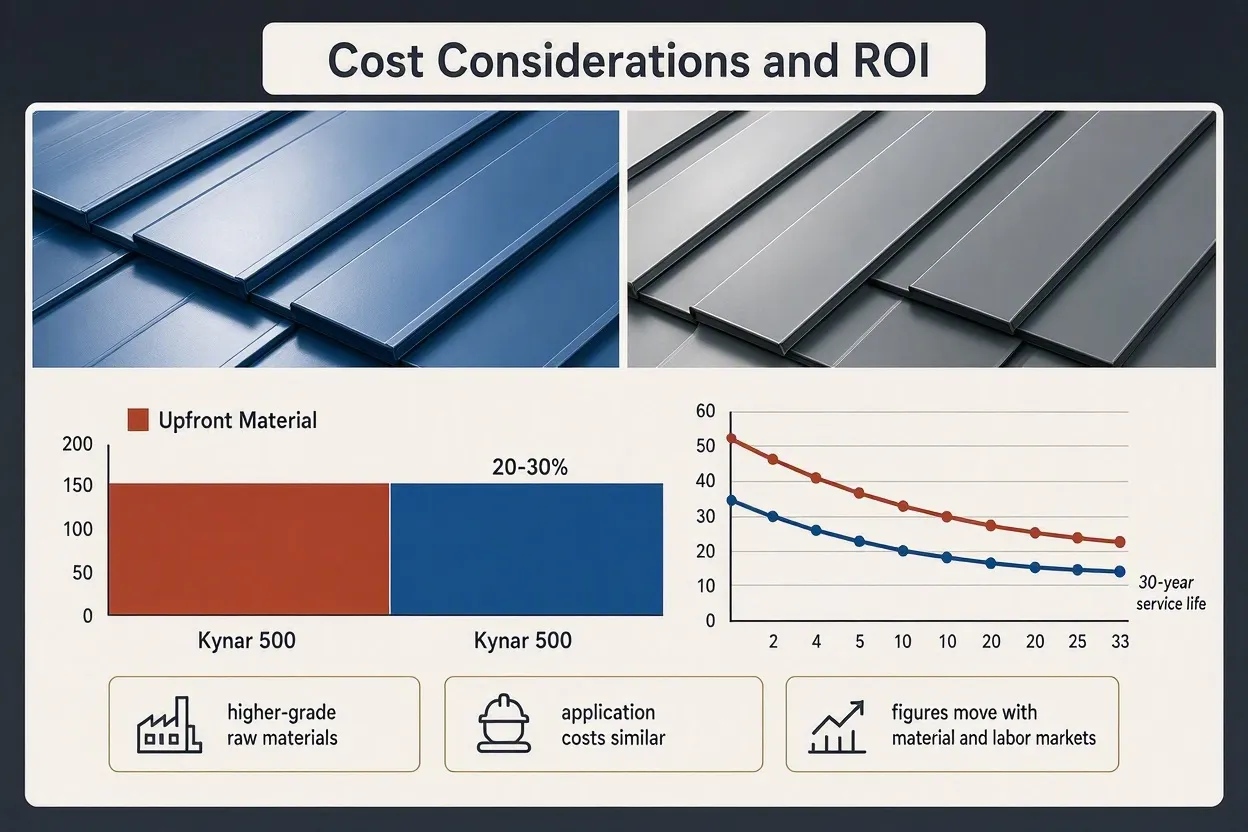
Kynar 500 costs more upfront than standard coatings, but the gap closes once material and labor markets are factored against the coating’s full 30-year service life. These figures move with material and labor markets, so treat them as directional rather than fixed.
Upfront costs:
- Material costs run 20-30% higher than standard coatings, driven by higher-grade raw materials and tighter manufacturing tolerances
- Application costs stay roughly in line with other high-performance systems, though certified applicators may charge a premium for their expertise
- Certification and testing fees add another $0.50-1.00 per square foot
Long-term savings:
- Skipping 2-3 full recoating cycles over 30 years saves an estimated $15-25 per square foot
- Energy savings of 15-25% on cooling costs can add up to thousands of dollars a year for large buildings
- Maintenance costs run roughly 60% lower than standard coatings
- Buildings coated with premium systems tend to see a 2-5% bump in property value
Warranty value:
- Coverage for color fade, chalking, and adhesion typically runs 30 years, well beyond industry norms
- The warranty is often transferable, which helps at resale
- Claims are rare, but the process is straightforward when they do come up
Project size factors:
- Volume discounts kick in around 10,000 square feet, cutting per-unit costs 10-15%
- Standard colors cost less than custom matches
- Custom color matching adds $500-2,000 in development and testing fees to get an exact aesthetic match
FAQs
Is Kynar 500 the same as PVDF coating?
Yes. Kynar 500 is a brand name for a coating system built on PVDF (polyvinylidene fluoride) resin, manufactured by Arkema. Other brands, like Hylar 5000, use PVDF resin too, so “Kynar 500” and “PVDF coating” are often used interchangeably, but Kynar 500 specifically refers to Arkema’s formulation.
How long does Kynar 500 last on a metal roof?
Kynar 500 lasts 30-40 years on a metal roof under normal conditions. The coating typically carries a 30-year warranty against fade, chalking, and adhesion failure, and it holds up to 80% of its original gloss after two decades.
Does Kynar 500 cost more than standard paint?
Yes. Kynar 500 costs 20-30% more than standard coatings at installation. That gap closes over the coating’s lifespan, since Kynar 500 eliminates 2-3 recoating cycles over 30 years and cuts maintenance costs by around 60%, which brings total lifecycle cost 40-60% below standard systems.
Can Kynar 500 be applied in the field, or does it require a factory?
Kynar 500 can be applied both ways. Coil coating happens in a factory setting through a continuous process, which gives the most uniform results for flat stock. Spray application works on-site for complex geometries, but it requires experienced applicators and a controlled environment to hit the same performance standards.
What is the minimum PVDF content for a coating to be called Kynar 500?
A coating needs a minimum of 70% PVDF resin to qualify as Kynar 500. That threshold matters because performance drops sharply below it: coatings with 50% PVDF last only half as long, and anything under 30% offers little advantage over traditional paint.
Conclusion
Kynar 500 sits at the top of the coatings market for a reason. Its weather resistance, chemical resistance, and 30-year color retention deliver protection that standard coatings can’t match, which is why it’s the standard choice for projects that need to last.